A 0402 capacitor can look intact, pass a quick visual check, and still be the reason a board will not boot. SMT testing is the discipline of finding that failure without damaging adjacent parts, misreading an in-circuit value, or spending an hour probing a circuit that should have been isolated in minutes.
For assembly teams, repair technicians, and engineers, the challenge is not simply measuring resistance, capacitance, or voltage. It is deciding what to measure, where to measure it, and whether the reading represents the component itself or the circuit around it. Good SMT testing combines inspection, controlled electrical measurement, and comparison against known-good values or board data.
What SMT Testing Must Verify
Surface-mount technology places components close together, often beneath shields, connectors, or dense IC packages. That density improves product size and performance, but it also changes the test process. Leads are too small for conventional clips, solder joints can be hidden, and nearby parallel paths can affect in-circuit readings.
A useful test process verifies four different conditions: the correct component is installed, it has the correct value, its solder connections are sound, and it behaves correctly within the powered circuit. These are related but not interchangeable. A component may have the right marking and nominal value but be cracked. A perfect solder joint may connect the wrong resistor reel value. A capacitor can measure normally with power removed yet fail only when bias voltage is applied.
The right test method depends on where the board is in its life cycle. Incoming inspection focuses on component identity and lot quality. Production inspection looks for placement and soldering defects. Repair work starts with symptoms and narrows toward the defective section. Each stage benefits from fast access to reliable component measurements.
Start With Inspection Before Measurement
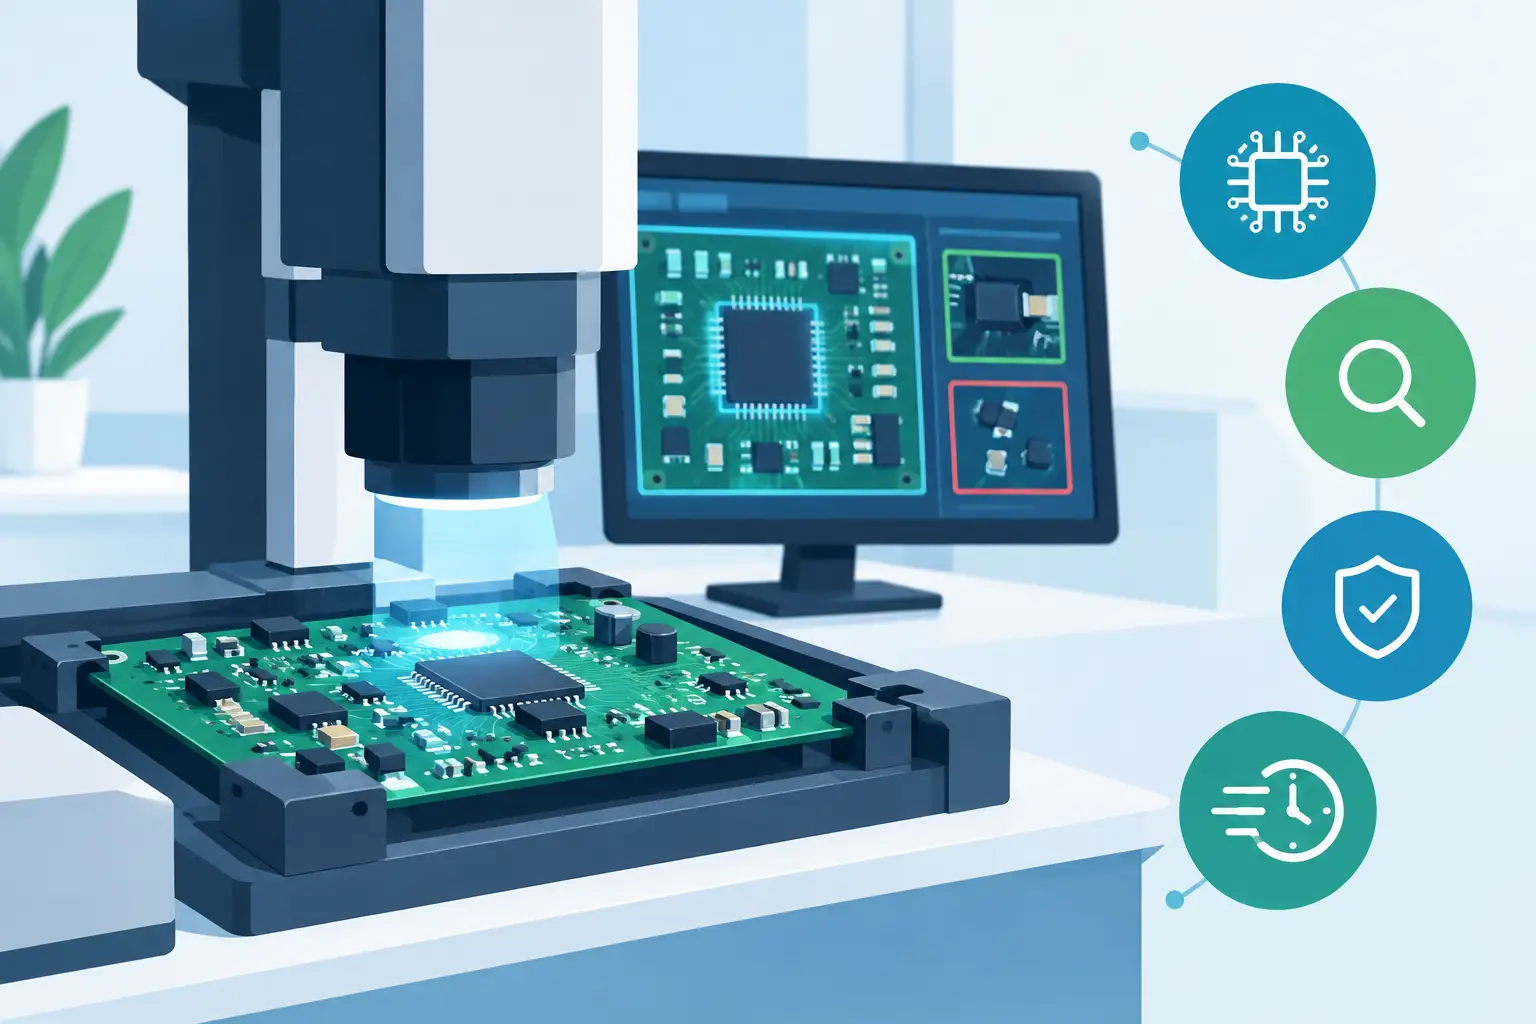
Electrical measurement should not replace visual inspection. Before applying probes, inspect the board under sufficient magnification and lighting. Look for tombstoned chip components, skewed packages, incomplete fillets, solder bridges, lifted pads, cracked ceramic capacitors, damaged inductors, and signs of overheating.
Pay close attention to polarized parts. Reversed tantalum capacitors, diodes, LEDs, and polarized ICs can create immediate power faults. Also check for wrong-package substitutions. A 0603 part placed where an 0402 was specified may be physically obvious, but an incorrect value resistor in the correct package usually is not.
Automated optical inspection is effective for placement and visible solder defects in volume production. It does not prove an installed resistor is the specified value or that a capacitor has acceptable ESR. Electrical testing remains necessary when visual inspection reaches its limit.
Choose the Right SMT Testing Method
No single instrument or process answers every question. The most efficient approach uses the simplest test that can confirm or eliminate a suspected failure.
Power-Off Component Checks
With the board unpowered and discharged, measure resistors, capacitors, inductors, diodes, and obvious shorts. This is often the fastest way to identify a failed passive component or confirm a questionable part before deeper diagnosis.
Tweezer-style LCR meters are particularly useful for chip components because both contacts can be reached directly without test leads slipping across neighboring pads. An automatic meter that identifies resistance, capacitance, or inductance reduces manual range selection and helps maintain a consistent workflow from one component to the next.
However, an in-circuit measurement is not automatically a component value. A resistor may read low because another resistor is in parallel. A capacitor may read high because it is connected to other capacitance on the rail. An inductor may measure nearly as a short because its DC resistance is intentionally low. When the reading does not match the schematic or bill of materials, isolate one end of the component if practical and measure again.
Continuity and Short-Circuit Checks
Continuity testing is valuable for verifying traces, vias, fuses, zero-ohm links, and soldered connections. It is also a fast first check on a dead power rail. Measure resistance from the rail to ground and compare it to a known-good board when available.
A low resistance reading is not always a fault. Core-voltage rails, processors, memory devices, and power-management circuits can present low resistance by design. The meaningful question is whether the reading is abnormal for that rail and board revision. Comparison is more reliable than assuming every low-ohm rail is shorted.
Powered Voltage and Signal Checks
When power-off checks do not identify the issue, move to controlled powered testing. Verify input voltage, regulator outputs, enable pins, reference voltages, and reset lines. A digital multimeter is useful for DC rails, while an oscilloscope is required when ripple, switching activity, clock signals, or intermittent behavior is suspected.
Use fine probes, insulation sleeves, or appropriate test fixtures when working on dense assemblies. One accidental probe slip can bridge adjacent IC pins and create a second fault that masks the original one. Current-limited power supplies are equally important during initial fault finding, especially where a shorted capacitor or damaged IC may draw excessive current.
Measuring Common Surface-Mount Components
Passive components cause a large share of board-level failures because they are numerous, small, and exposed to heat and mechanical stress. Their readings must be interpreted in context.
| Component | Primary check | Common interpretation issue | |—|—|—| | Resistor | Resistance | Parallel circuit paths produce a lower reading | | Capacitor | Capacitance and ESR | In-circuit capacitance may include other capacitors on the rail | | Inductor | Inductance and DC resistance | Low resistance is often normal for power inductors | | Diode or LED | Forward voltage and polarity | Parallel semiconductors can alter diode-mode readings | | Ferrite bead | Continuity or low DC resistance | It may look like a short at DC but filter high-frequency noise |
For ceramic capacitors, visible cracking near the board edge, mounting hole, or heavy connector is a frequent concern. Board flexing can fracture the ceramic body or its internal terminations. A cracked MLCC may become leaky or shorted only under voltage, so a capacitance reading alone may not settle the diagnosis.
ESR testing matters most with electrolytic and polymer capacitors, but it can also help establish whether a capacitor is behaving unexpectedly in a circuit. Test frequency matters. A capacitance result taken at one frequency may differ from a result at another, particularly with inductive, high-value, or low-quality components. Use the test conditions specified by the component data when verification requires tight tolerance.
Build a Repeatable Diagnostic Sequence
A repeatable sequence prevents random probing and makes results easier to document. Begin with the fault symptom, then identify the associated power domain, functional block, or signal path. Compare against schematics, board layout, assembly drawings, or a known-good unit whenever possible.
For an unpowered board, first inspect for mechanical damage and solder defects. Next, check main rails for abnormal resistance to ground, then evaluate the components most directly connected to the suspect rail. If the board powers but fails functionally, confirm each supply voltage before replacing logic devices. A missing or unstable regulator output can mimic failures in processors, memory, displays, radios, and sensors.
Keep a record of readings that matter: board serial number, test point, instrument mode, measured value, and component reference designator. This is particularly useful in recurring repair work. Patterns such as repeated failures of the same input capacitor, protection diode, or regulator can reveal a design stress issue, handling problem, or supplier variation.
Accuracy Depends on Contact and Calibration
A high-quality meter cannot compensate for poor probe contact. Oxidation, flux residue, conformal coating, and uneven solder fillets can create unstable readings. Clean the test location when appropriate, hold the contacts squarely on the component terminations, and wait for the measurement to settle before recording it.
For low-resistance and low-ESR work, lead and contact resistance can become significant. Kelvin connections separate the current path from the voltage-sensing path, reducing errors caused by probe resistance. This is especially relevant when checking milliohm-range shunts, low-resistance inductors, and high-current paths.
Instrument calibration should match the level of confidence the work requires. Routine bench troubleshooting may need periodic verification against known standards. Quality-control, production, and documented repair environments may require traceable calibration records. A calibrated handheld instrument such as an LCR-Reader can provide rapid component identification at the board, but calibration status and proper handling still determine whether the result is defensible.
When to Remove a Component
Removing a part is not a failure of the test process. It is the correct next step when circuit interactions prevent a confident in-circuit conclusion. Lift one termination rather than fully removing the component when the goal is simply to eliminate parallel paths. This limits rework stress and preserves the original placement reference.
Removal has trade-offs. Excess heat can damage pads, nearby components, or multilayer-board connections. It also introduces the possibility of an intermittent fault disappearing during rework. Before desoldering, document the original orientation and take enough measurements to explain why isolation is necessary.
The best SMT testing decisions are usually made before the probes touch the board: know the expected behavior, select the measurement conditions, and treat every reading as evidence rather than a verdict. That discipline turns a compact meter and a steady pair of hands into a faster, more reliable repair process.