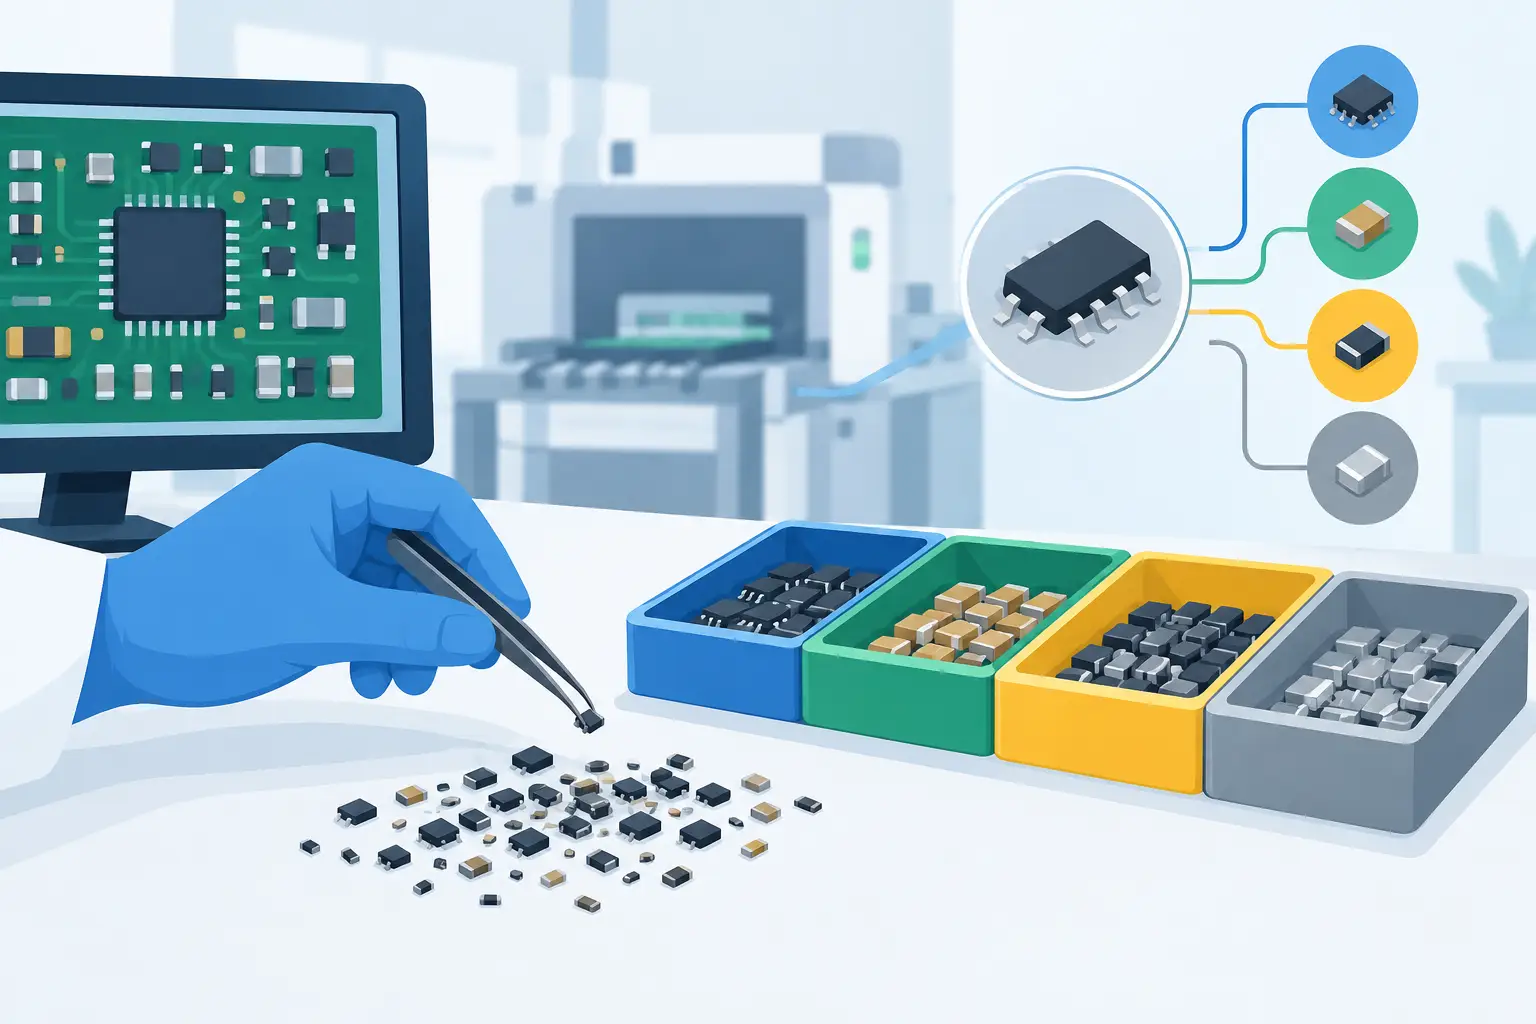
A mixed tray of 0402 capacitors, resistors, and inductors can stop an otherwise routine repair or assembly job. Package markings may be absent, tape labels may be incomplete, and visually similar parts can have entirely different electrical functions. Effective component sorting turns that uncertainty into a controlled verification process: identify the part, measure it under suitable conditions, separate it clearly, and record exceptions before they reach a board.
For SMT rework, incoming inspection, salvage, and prototype assembly, sorting is not merely an organizational task. It is a quality-control step. A resistor placed in a capacitor bin can often be caught quickly. Two ceramic capacitors with the same package and different values are more difficult, especially when their markings provide no useful information. Measurement at the bench is what makes the difference.
Why component sorting requires electrical verification
Physical appearance is useful only as a first filter. Package size, body color, end caps, and reel label format can narrow the possibilities, but none of them confirm value or component type. A 0603 capacitor and a 0603 resistor may appear nearly identical at a glance. Inductors, ferrite beads, and some low-value resistors can also be confused when they are loose or poorly marked.
Electrical measurement provides the confirmation. Resistance identifies resistors and can expose a shorted part. Capacitance separates capacitor values. Inductance helps distinguish inductors from other two-terminal components. ESR adds another layer of screening for capacitors, particularly when evaluating used stock or parts removed from assemblies.
The practical goal is not to force every part through an extended lab characterization. The goal is to make a reliable sorting decision quickly enough that the process improves throughput rather than creating a bottleneck.
Start with a sorting workflow that prevents rework
A good workflow separates visual triage from measurement. Begin by dividing parts according to package family and any available markings. Keep unknown components isolated from known inventory. If parts arrived on cut tape, preserve the original label with the strip whenever possible, even after an electrical check.
Next, measure one representative part from a suspected group. If the reading matches the label or expected value, measure several additional samples before accepting the lot. A single correct reading does not prove that a mixed tray or reel segment is uniform. For high-risk material, such as salvaged components or parts returned from a production area, sample more aggressively or measure every item.
Once confirmed, place parts in labeled compartments, tape them to a card, or return them to properly identified carrier tape. The label should include the electrical value, tolerance if known, package size, and any condition note such as “removed stock” or “unverified temperature coefficient.” This distinction matters because a measured 10 uF capacitor is not necessarily interchangeable with every 10 uF capacitor specified on a bill of materials.
Choose measurements that match the component
Automatic component identification is highly useful during general sorting because it reduces instrument setup and helps the operator move between resistors, capacitors, and inductors without changing modes. For loose SMT components, tweezer-style contacts also eliminate the need for clips or fixture leads that can slow handling and add instability to low-value readings.
That said, the measured result must be interpreted in context. A resistance reading is generally straightforward for a resistor, but low-ohm values demand attention to probe contact resistance and lead compensation. A capacitor’s measured value depends on test frequency, applied signal level, dielectric type, DC bias conditions, and measurement method. Inductors may require a test frequency that reflects how the part will be used.
For routine identification, automatic settings are often sufficient. For borderline values, unusual parts, or acceptance testing, use a meter that provides the necessary test-frequency control and measurement resolution. The best setting is not always the highest frequency or the fastest reading. It is the setting that gives a stable, repeatable result appropriate to the component and specification.
Resistors: check value and contact quality
Resistor sorting is usually the fastest category, provided the contacts are clean. Hold the component firmly at both terminations and wait for the reading to settle. If a low-value resistor reads higher than expected, verify the contact surfaces before rejecting it. Oxidation, solder residue, weak tweezer pressure, and dirty probe tips can all add error.
For very low resistance values, compensation and Kelvin-style measurement techniques become more significant. A reading that is acceptable for identifying a 10 kOhm resistor may not be sufficient to distinguish a 0.10 ohm current-sense resistor from a 0.12 ohm part. Sort these parts into a dedicated low-resistance workflow instead of treating them like general-purpose chip resistors.
Capacitors: value alone is not the full answer
Capacitor sorting often produces the most uncertainty because unmarked MLCCs are common and capacitance changes with conditions. High-capacitance Class 2 ceramic capacitors can vary significantly with DC bias, temperature, age, and test voltage. A result slightly below the nominal marking does not automatically mean the component is defective.
Use capacitance measurement to separate obvious groups, then compare readings against the expected tolerance and the meter’s test conditions. ESR can provide additional screening where relevant, particularly for electrolytic or polymer capacitors. It is less useful as a universal pass-fail criterion for every ceramic capacitor.
Keep dielectric-sensitive parts separate when the application requires it. A 1 uF X7R MLCC and a 1 uF C0G capacitor may measure similarly at the bench, yet behave very differently in a precision timing, RF, or high-bias circuit.
Inductors and ferrite beads: avoid false assumptions
Inductors should be sorted by inductance, package, current rating, and DC resistance when those characteristics matter. Two inductors with similar inductance may have substantially different saturation-current ratings or losses. Measurement confirms the nominal inductance, but it does not replace the manufacturer’s specification for power applications.
Ferrite beads require special care. Their impedance is frequency-dependent, and a basic inductance reading may not describe their intended noise-suppression performance. Sort beads separately from power inductors and retain any available manufacturer identification. If the part must meet an EMI requirement, use the original specification rather than substituting based on a single low-frequency measurement.
Control the factors that create bad readings
Many sorting errors come from technique rather than the meter. Components should be clean, dry, and disconnected from any circuit. Probe tips must make solid contact at the metal terminations, not the component body or solder residue. For tiny parts, a stable hand position matters because movement changes contact pressure and can interrupt the measurement.
Instrument condition matters as well. Verify calibration status and perform the recommended open and short compensation procedure when the device and measurement range require it. Inspect tweezer tips for wear, contamination, or damage. A precision meter cannot compensate for a bent tip that touches inconsistently.
Environmental conditions are another consideration for precision work. Temperature changes can affect both the component and the instrument. In a general repair setting, this may not be consequential. In incoming inspection of tight-tolerance resistors or reference capacitors, allow parts and equipment to stabilize before making final acceptance decisions.
Build a practical component sorting station
An efficient station keeps the measurement path short: incoming parts, meter, labeled containers, and a record sheet or inventory system should be within reach. Avoid creating a large “to be sorted” pile with no clear status. Use separate areas for unmeasured parts, verified parts, rejects, and parts requiring further review.
For high-volume loose SMT work, a handheld auto-identifying LCR meter such as an LCR-Reader can reduce handling time by measuring directly with tweezer probes. This approach is especially useful when technicians need to identify components removed during troubleshooting or verify a part before installation. For advanced screening, select an instrument with the required ranges, accuracy, test frequencies, and calibration support rather than relying on convenience alone.
Documenting results does not need to be complicated. Record the part type, measured nominal value, quantity, package, source, and any limitations. A note such as “measured 4.7 uF, dielectric unknown” is more useful than labeling a bin simply “4.7 uF.” It preserves the uncertainty that could matter later.
When sorting should stop and analysis should begin
Some components cannot be reliably approved through basic LCR measurement alone. Semiconductors, transient suppressors, thermistors, crystals, RF parts, and specialized networks may need different test methods. Even passive parts may require datasheet review when voltage rating, tolerance, dielectric, current capacity, pulse performance, or frequency behavior is critical.
Treat component sorting as a decision process, not a promise that every electrical property has been verified. Measure what is needed to prevent mix-ups, then escalate parts that affect safety, performance margins, or production compliance.
A well-organized bin saves time. A verified bin protects the board, the repair schedule, and the next technician who has to trust what is inside.