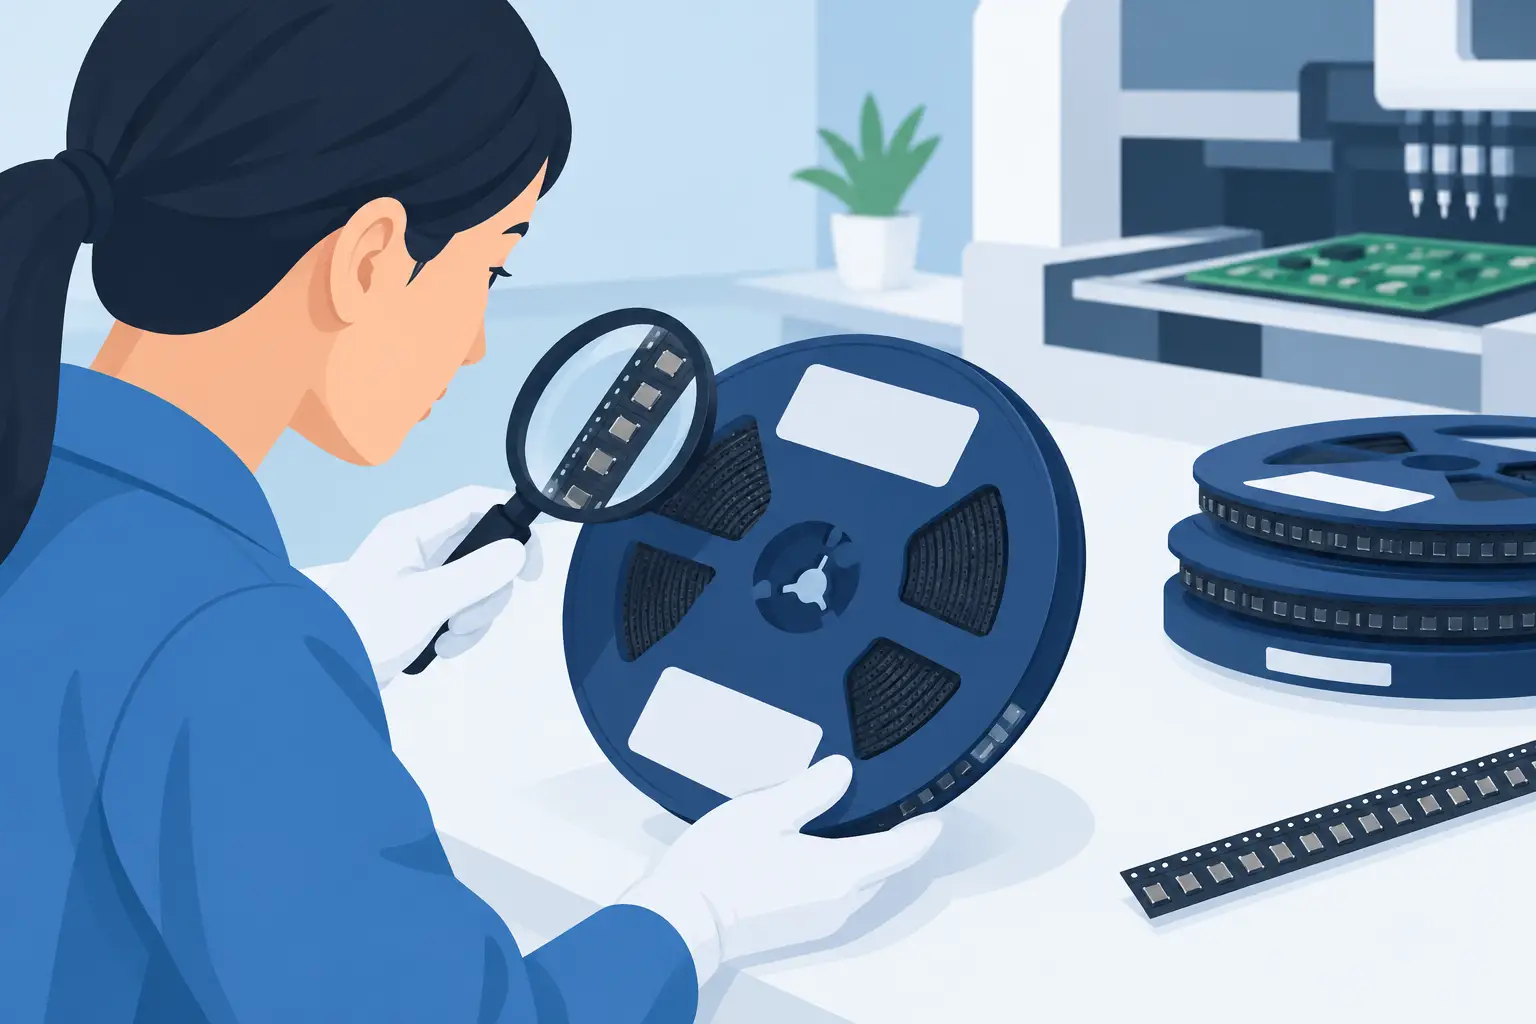
A reel marked 10 kOhm can still create a costly assembly error. A transposed digit in a distributor label, an incorrect internal barcode association, or a reel returned to the wrong bin can place a nearly identical part on the line. Verifying resistor reel labels before loading feeders or beginning a repair is a small control step that prevents rework, scrap, and difficult-to-trace field failures.
For SMT work, the label is the starting point, not the proof. A reliable verification process compares the reel label with the purchase record, manufacturer data, package requirements, and a measured sample. The depth of that process should match the risk: a prototype bench build and a high-volume production run do not need the same sampling plan, but neither should rely on color, memory, or a quick visual check.
What a Resistor Reel Label Should Confirm
A complete reel label identifies more than nominal resistance. At minimum, it should let the technician or operator confirm the manufacturer part number, resistance value, tolerance, package size, temperature coefficient when specified, reel quantity, and lot or date code. Some labels also state power rating, thick-film or thin-film construction, termination type, and moisture sensitivity information for associated packaging.
The manufacturer part number is usually the most useful control point. It ties the physical reel to an approved bill of materials and manufacturer datasheet. A label that says only “4.7 k” is not enough where multiple approved 4.7 kOhm resistors have different tolerances, package sizes, pulse ratings, or temperature coefficients.
Package designation deserves the same attention as value. A 0402 resistor and a 0603 resistor can carry the same nominal resistance, but they are not interchangeable unless the footprint, power dissipation, placement program, and design requirements allow it. Metric and imperial package references can also cause confusion. Confirm the actual manufacturer package code rather than assuming every supplier uses the same notation.
Decode the value carefully
Most reel labels print resistance in a direct format such as 100 Ohm, 1 kOhm, 10 kOhm, or 1 Mohm. Others use a three- or four-digit code. For example, 103 commonly represents 10,000 Ohms, while 1001 represents 1,000 Ohms in a four-digit system. The letter R is used as a decimal marker, so 4R7 means 4.7 Ohms and 0R0 is a zero-ohm link.
Do not assume the printed code alone establishes the part value. Marking conventions differ for precision parts, arrays, jumpers, and components supplied under internal inventory numbers. Cross-check the code against the manufacturer part number or approved component record.
A Practical Process for Verifying Resistor Reel Labels
Start with documentation, then use measurement to confirm the physical material. This order is faster than attempting to identify every reel from a resistance reading alone, especially when several values are close together.
First, compare the reel part number to the BOM, approved vendor list, or work order. Confirm that the specified resistance, tolerance, package, and power or voltage rating match the intended reference designator. If the assembly calls for a 1% resistor, a 5% reel with the same nominal value is not automatically acceptable.
Next, inspect the reel and packaging for evidence of handling errors. Check whether the original manufacturer label is present, whether a distributor or internal label covers critical information, and whether the reel has been partially used. A partial reel may be legitimate, but it requires stronger traceability. The leader tape, cover tape, pocket orientation, and component body size should agree with the feeder setup and package requirement.
Then measure representative parts. Remove a component from the reel only when your process permits it, and avoid pulling a sample from the leader where a previous operator may have placed a substitute part. Measure several parts from different points in the reel when the reel has been opened, relabeled, returned to stock, or received from an unfamiliar source.
For common chip resistors, a handheld tweezer-style LCR meter can identify resistance directly at the component terminals without building a separate fixture. This is particularly useful for incoming inspection, feeder setup, and repair benches where a conventional meter probe can slip on 0402 or 0201 parts. Clean contacts and stable pressure matter. Oxidation, flux residue, or a poor probe connection can make a low-value measurement appear incorrect.
Finally, record the result in the inventory or production system. The record should associate the internal stock number with the original manufacturer part number, measured result, lot information, date, operator, and disposition. If the reel passes, apply an internal verification status only if that is part of the documented quality process. If it fails, quarantine it rather than relabeling it based on assumption.
Measure the Right Way When Verifying Resistor Reel Labels
Measurement confirms resistance, but it does not independently confirm every electrical characteristic. A 10 kOhm 1% resistor and a 10 kOhm 5% resistor may both measure close to 10 kOhm at room temperature. Likewise, two resistors with different pulse ratings or temperature coefficients can look identical in a basic resistance check. Measurement must support the label review, not replace it.
For values above a few hundred Ohms, ordinary two-wire resistance measurement is generally adequate for identifying the nominal value. For low-value resistors, contact resistance becomes a major source of error. A 0.1 Ohm shunt resistor cannot be verified confidently if probe and contact resistance are a significant fraction of the reading. Use a Kelvin connection or an instrument and fixture designed for low-resistance measurement when the application requires it.
Keep tolerance in perspective. A nominal 1 kOhm resistor with 1% tolerance may measure from 990 to 1,010 Ohms under the specified conditions. A reading of 997 Ohms supports the identification. A reading of 1.00 kOhm does not prove the component is a specific tolerance grade, manufacturer, or temperature coefficient.
Capacitive effects from tape, contamination, or nearby conductive surfaces can also affect readings on small components. Measure the resistor outside the pocket when possible, use clean tweezer tips, and allow the reading to stabilize. For precision or low-ohm components, verify the instrument calibration status and use the appropriate calibration fixture or procedure before making an acceptance decision.
Common Causes of Reel Identification Errors
The most frequent errors are operational, not mathematical. Reels are often mixed after a feeder change, returned to inventory under the wrong stock number, or relabeled after a receiving discrepancy. Similar values create another problem: 10 kOhm, 100 kOhm, and 1 kOhm can all appear in the same design, while 4.7 kOhm and 47 kOhm differ by only one character on a small label.
Substitutions require special control. An approved alternate may have the correct resistance and package but a different manufacturer part number, tolerance, or reel orientation. It should be verified against the approved alternate record, not against the original part label. Treating all same-value resistors as interchangeable can cause failures in precision dividers, current-sense circuits, analog feedback paths, and high-voltage designs.
Counterfeit or salvaged material is another reason to verify more than one field on the label. Warning signs include inconsistent fonts, labels with incomplete part numbers, unexplained over-labeling, missing lot traceability, unusual pocket dimensions, or readings that vary widely across samples. These signs do not prove a reel is defective, but they justify holding the material for a more thorough review.
Set Verification Depth by Risk
A practical inspection plan is not identical for every reel. For a low-cost prototype using general-purpose 5% resistors from controlled stock, confirming the internal stock number, package, and a measured sample may be sufficient. For production material used in a precision, safety-related, medical, or automotive assembly, the process may require documented lot traceability, multiple samples, calibrated measurement equipment, and quality approval.
The same principle applies to rework. Before replacing a resistor on a dense board, confirm the intended value from the schematic or board documentation, then measure the replacement part before installation. Measuring a resistor in circuit can be misleading because parallel paths alter the result. If the value is critical and the circuit is ambiguous, isolate one end of the component or use the design documentation as the primary source.
Treat a reel label as controlled technical data, not packaging decoration. A short comparison of part number, package, tolerance, and measured value at the bench is far easier than finding a resistor mix-up after hundreds of boards have passed through assembly.